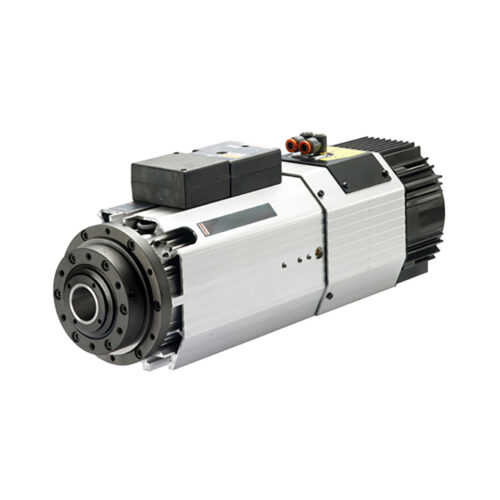


Perske KNS61-13-2DS Spindle Motor
$5,405.71
Perske KNS61-13-2DS high-precision, double-ended 7 HP (5.2 kW) manual tool change (MTC) spindle motor is engineered for continuous-duty CNC routing and heavy-duty machining applications. Operating at 18,000 RPM (300 Hz), it delivers high torsional rigidity and tight runout tolerances.
Only 1 left in stock
Description
The Perske KNS61-13-2DS high-frequency spindle motor delivers industrial-grade performance for precision CNC routing, wood processing, and non-ferrous metal cutting. Engineered by Perske in Germany, this 2-pole, dual-voltage (220V/380V) electric spindle produces 7.0 HP (5.2 kW) at its rated operating frequency of 300 Hz.
Featuring a double-ended shaft design with integrated manual tool change capabilities, the KNS61-13-2DS uses standard SYOZ 20 / OZ 1833 collet retention systems to provide maximum radial stiffness and minimal Total Indicated Runout (TIR). The motor is self-cooled via an integrated shaft-driven fan assembly, ensuring thermal stability during extended continuous-duty production cycles.
Technical Specifications
- Model / Type: Perske KNS 61 / KNS61-13-2DS
- Tool Change: Manual Tool Change (MTC)
- Tool Interface:
- SYOZ 20, OZ 1833, or EOC 12 collets
- 1/2 inch max tool capacity
- OZ 1822 cover nut 83634
- Cooling: Self-cooled by integrated fan
- Max Speed: 18,000 RPM
- Frequency: 300 Hz
- Pole Count: 2-pole
- Power: 7 hp (5.2 kW)
- Voltage: 220 V or 380 V (Dual Voltage)
Additional information
| Manufacturer | Perske |
|---|---|
| Country/Region of Manufacture | Germany |
| Model Series | |
| Part Number (MPN) | KNS61-13-2DS, KNS 61.13-2 |
| Tool Change | |
| Collet size | SYOZ 20, OZ 1833, EOC 12 |
| Cooling Method | Fan Cooled |
| Speed (RPM) | 18,000 |
| Output Frequency (Hz) | 300 |
| Poles | 2 |
| Kilowatt (kW) | 5.2 |
| Horsepower (hp) | 7 |
| Voltage (V) | 220, 380 |
| Condition | New |
Common Failure Modes & Troubleshooting
Operating under high RPMs and thermal loads, precision spindles require proactive monitoring to prevent unexpected machinery downtime.
Bearing Wear / Vibration
Caused by unbalanced tooling or axial overloading. Inspect runout regularly; replacement requires angular contact bearings rated for 18,000+ RPM.
Overheating
Caused by airflow restrictions or incorrect VFD V/Hz configuration. Set VFD base frequency strictly to 300 Hz to protect winding insulation.
Collet Binding & Taper Contamination
Debris in the inner taper elevates runout. Clean tapers with precision swabs during every tool change.
If you detect excess vibration, thermal spikes, or abnormal noise, immediate diagnostics can prevent permanent shaft and rotor damage. Contact our technical team for expert troubleshooting support and specialized CNC router repair services.